

News
- ▶ How alloy bar stock size affects material yield in machining
- ▶ Which ultrasonic inspection standard applies to critical alloy bar
- ▶ Why alloy bar can develop cracks during hot forging
- ▶ What to check before buying alloy bar for pressure equipment
- ▶ How alloy bar grain structure affects fatigue resistance
Message
How alloy bar stock size affects material yield in machining
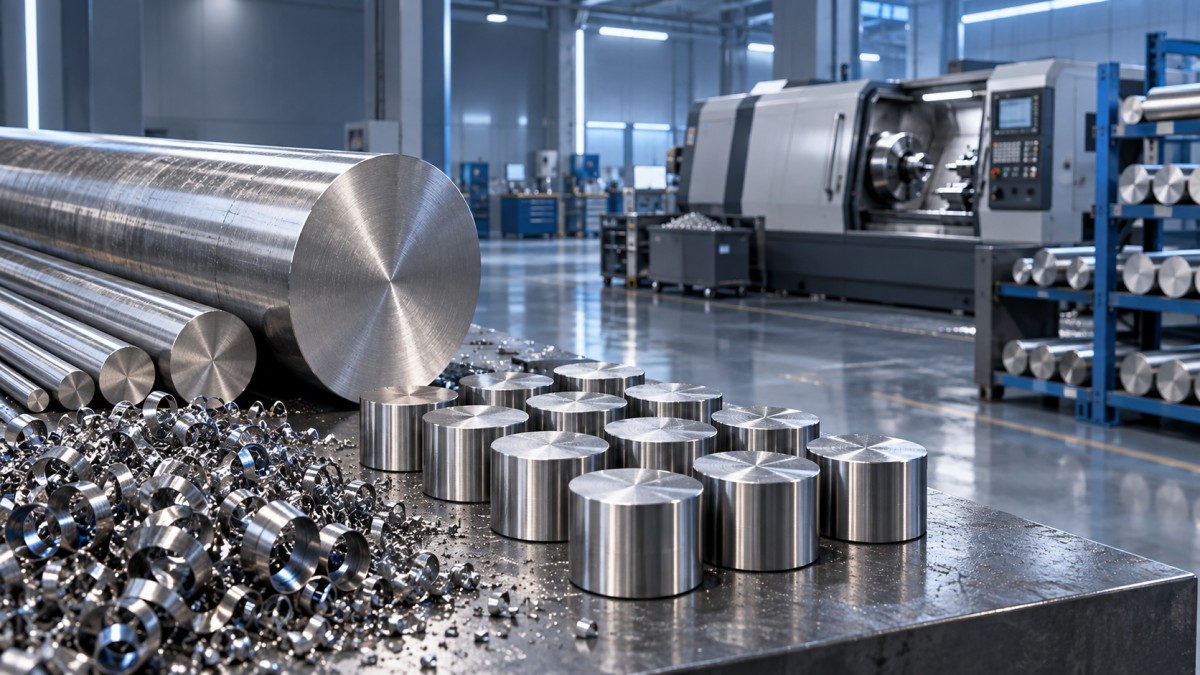
A machining quote can appear competitive until the material balance is reviewed. A part may be small, yet an oversized starting bar can leave a large annular ring of chips, increase cutting time, and raise the amount of high-value alloy that never reaches the finished component. The opposite choice can also create trouble: a bar selected too close to the finished envelope may not provide enough machining allowance to remove scale, decarburized surface, ovality, or handling damage.
The practical answer is that Alloy Bar size affects yield through three linked factors: the ratio of finished-part volume to starting-stock volume, the material allowance required by the process, and the losses created by bar ends, kerf cuts, and remnant lengths. The best size is not simply the smallest available diameter. It is the smallest qualified diameter and length that still supports reliable machining, fixturing, inspection, and material traceability.
Where yield is lost before machining even begins
Material yield is often discussed as the percentage of purchased material that becomes a finished part. In a turning operation, the main loss is usually the difference between the stock diameter and the largest finished outside diameter. Since round-bar volume rises with the square of diameter, a modest increase in starting diameter can create a disproportionate increase in removed material.
For example, a cylindrical component with a relatively small finished outside diameter may be machined from a much larger standard bar because that is what is readily available. The extra stock does not only become chips. It also requires additional roughing passes, consumes inserts, adds machine hours, and may increase distortion risk in materials that work-harden or retain residual stress. Nickel-based, cobalt-based, titanium, and corrosion-resistant alloys make this effect more commercially significant because their raw-material value and machining difficulty are both higher than for ordinary carbon steel.
Length is equally important but easier to overlook. A long bar may have a lower unit price, yet poor cut planning can produce short remnants that cannot be assigned to another order. Each cut also consumes saw kerf, and facing operations remove material from both ends of every blank. When order quantities are limited, these fixed losses can represent a meaningful share of the purchased length.
Diameter selection: balance allowance against chip volume
The evaluation should begin with the part’s maximum machined diameter, not its nominal diameter alone. Identify any flange, shoulder, interrupted feature, or runout condition that defines the true starting envelope. Then determine the allowance needed to remove the supplied surface and establish a stable reference diameter.
Allowance depends on the delivered condition of the bar. Hot-worked material may need more cleanup than cold-finished or precision-ground material. Diameter tolerance, straightness, surface condition, and the intended machining route all change the answer. A part that will be rough-turned and finish-turned can tolerate a different starting condition from a part that needs only light finishing before threading or milling.
A useful commercial discipline is to compare candidate diameters by net usable mass per finished part, rather than comparing price per kilogram alone. The calculation should include expected machining allowance, the actual bar tolerance band, and the finished geometry. It should also distinguish recoverable scrap from nonrecoverable loss. Turnings may retain some recycling value, but that value is rarely equivalent to certified, traceable bar stock.
Length planning can change the quote more than expected
A shop may receive bar in standard mill lengths and then cut it into blanks. The ideal purchased length is therefore connected to the blank length, the saw kerf, facing allowance, clamp allowance, and the number of pieces that fit from each bar. A one-piece difference per bar can materially alter utilization, especially where the order involves expensive alloys or relatively short components.
Before approving a material plan, map the cut pattern rather than using a simple purchased-length-to-part-length ratio. Include:
- blank length, including facing stock and any required chuck or collet grip;
- saw kerf for every separation cut;
- the unusable crop at the beginning and end of the bar;
- length lost where identification marks, surface defects, or end damage must be removed;
- the minimum remnant length that the shop can realistically reuse.
Longer bars tend to reduce the proportion of end loss, but they can introduce handling and straightness concerns. They may also be impractical for machines with limited bar-feed capacity. Short cut blanks reduce handling complexity and can suit machining centers, but the increased number of saw cuts and individual setups may offset part of the material advantage. The correct choice is tied to the production route, not merely the material purchase order.
Tolerances are a yield variable, not just a quality requirement
A nominal diameter does not tell the whole story. A wide positive tolerance may force the machinist to remove more material than the nominal calculation suggests. Conversely, a bar that trends near the lower side of its tolerance can leave insufficient cleanup allowance on features that must be concentric with the original stock surface. Straightness and roundness matter for the same reason: a bar that is slightly bowed or out-of-round may demand extra stock removal before a consistent machining datum can be established.
When evaluating a supplier quotation, ask for the actual supply condition and dimensional tolerance alongside nominal size. A lower-priced bar with broad tolerances can create a less favorable total cost than a more controlled size that reduces rough-machining demand. This is particularly relevant where parts have thin walls, narrow finishing allowances, or demanding concentricity requirements.
Do not confuse near-net stock with guaranteed lower cost
Near-net bar sizes can improve yield, but only when the size is consistently available and the process can use it without creating new risk. A nonstandard diameter may require a longer lead time, a larger purchase minimum, or a dedicated production lot. If the part demand is intermittent, the leftover quantity may become dead inventory. The evaluator should compare total usable material, inventory exposure, lead-time risk, and machining savings together.
Material behavior affects the value of every extra millimeter
Not all alloys respond to excess allowance in the same way. Materials with high work-hardening tendencies may require deliberate roughing strategies and stable cutting engagement. Extra stock can mean more opportunities for work-hardened surfaces, tool deflection, heat buildup, and interrupted cuts around complex features. Titanium and certain nickel alloys may also demand careful control of cutting parameters to avoid surface damage or rapid tool deterioration.
For that reason, a diameter that looks acceptable in a simple weight calculation may still be unattractive on the shop floor. Estimators should request input from machining personnel when a part has deep cavities, thin sections, long unsupported lengths, or demanding surface-integrity requirements. The target is not maximum theoretical material yield; it is predictable yield at an achievable cycle time.
Stock form should also match the geometry. Round bar is appropriate for turned components, shafts, fittings, and rotational parts. But a component that begins as a thin, flat precision feature may waste substantial material when cut from round stock. In that situation, sheet or strip can provide a more rational starting form. For applications involving formed electronic components, sensors, transformers, or stable flat sections, Precision Alloy Steel Strips are available in thicknesses from 0.1 mm to 3 mm and may reduce unnecessary removal where the design genuinely suits strip processing.
A practical review sequence before releasing material
Start with the released drawing and identify the largest raw-stock envelope, including all finished diameters, machining datums, and workholding needs. Next, define the minimum cleanup allowance based on supply condition rather than habit. Review at least two feasible bar diameters when availability permits, then calculate the expected blank weight and removed volume for each option.
After diameter selection, create a cutting layout using the actual supplied bar length. Count kerf, crop, facing, and reusable remnants. A remnant should only be credited when its dimensions, heat identification, condition, and likely future demand make reuse realistic. Treating every leftover piece as usable can make a material plan look better than it will be in production.
Finally, add the machining implication to the comparison. A slightly larger size may be justified when it provides secure clamping or accommodates distortion control. A tighter-tolerance, smaller bar may justify a higher purchase price when it eliminates a roughing pass or reduces tool consumption. Recording these assumptions in the quote makes later variance review more meaningful and prevents material yield from being judged solely by the purchase price of the bar.
The most reliable purchasing decision is therefore based on the finished-part envelope, stock condition, cut pattern, and machining route as one set of variables. Selecting bar size this way avoids the two expensive extremes: buying large standard stock simply because it is familiar, or chasing the smallest possible diameter without enough allowance to machine the part consistently.
