

News
- ▶ How Inconel 625 manufacturers control composition between heats
- ▶ What makes an Inconel 625 manufacturer suitable for sour service
- ▶ How alloy bar stock size affects material yield in machining
- ▶ Which ultrasonic inspection standard applies to critical alloy bar
- ▶ Why alloy bar can develop cracks during hot forging
Message
How Inconel 625 manufacturers control composition between heats
Composition control between Inconel 625 heats begins before melting and continues until the heat is released with a traceable chemical record. The objective is not simply to obtain a passing final analysis. Each heat must remain within the applicable composition limits while preserving the nickel-chromium-molybdenum-niobium balance that supports corrosion resistance, weldability, strength, and resistance to localized attack in chloride-bearing or reducing environments.
Small variations can be acceptable within a specification yet still matter when material is intended for demanding welded fabrications, seawater equipment, chemical-process components, or powder-based manufacturing. A dependable Inconel 625 Manufacturer therefore controls both the measured elemental values and the process conditions that can cause those values to drift.
Start with controlled charge materials
The chemistry of a heat cannot be corrected reliably if the incoming charge is uncertain. Primary nickel units, chromium-bearing additions, molybdenum sources, niobium-bearing additions, and revert material require clear identification and documented chemistry. Revert is especially sensitive: scrap labeled as a nickel alloy may contain material from a different grade, welding consumable residues, coatings, oil, or embedded foreign metal.
Segregation of scrap streams matters because several alloy families appear visually similar while carrying materially different levels of iron, cobalt, copper, titanium, aluminum, sulfur, or other residual elements. A mixed revert charge may produce a heat that appears close to target chemistry at first analysis but has limited room for corrective additions. Once a restricted residual is high, dilution may be the only practical correction, and that changes yield, cost, and melt planning.
Raw material certificates establish a starting point, but receiving control should also address physical identity. Container markings, lot boundaries, storage separation, and clean handling reduce the chance that an otherwise certified addition becomes mixed with the wrong stock before charging.
Control the melt path, not only the final ladle sample
Inconel 625 is commonly produced through controlled melting and refining routes selected for the required product form and cleanliness level. During melting, losses, pickup, volatilization, slag-metal reactions, and the addition sequence all affect the final balance. Chromium and reactive elements require particular attention where oxidation exposure is present. Carbon, sulfur, oxygen, and nitrogen are also process-sensitive because contamination can enter through charge condition, furnace atmosphere, refractories, slag practice, or inadequate deoxidation.
The order of additions is deliberate. High-value alloying elements are not necessarily added all at once at the beginning of the melt. Their recovery and distribution depend on bath temperature, stirring, oxygen potential, and the time available for dissolution. Late trimming can improve compositional accuracy, but it must still allow enough mixing time for the sample to represent the whole bath. A quick sample taken near an addition point may suggest a value that is not representative of the final heat.
Refining is also a balance between removing undesirable species and retaining intended alloy content. Aggressive treatment intended to lower impurities can alter oxidation losses or create excessive slag interaction. The correct process window is therefore established around the specified chemistry, furnace capability, and required product route rather than around one isolated element.
Use analysis as a control loop
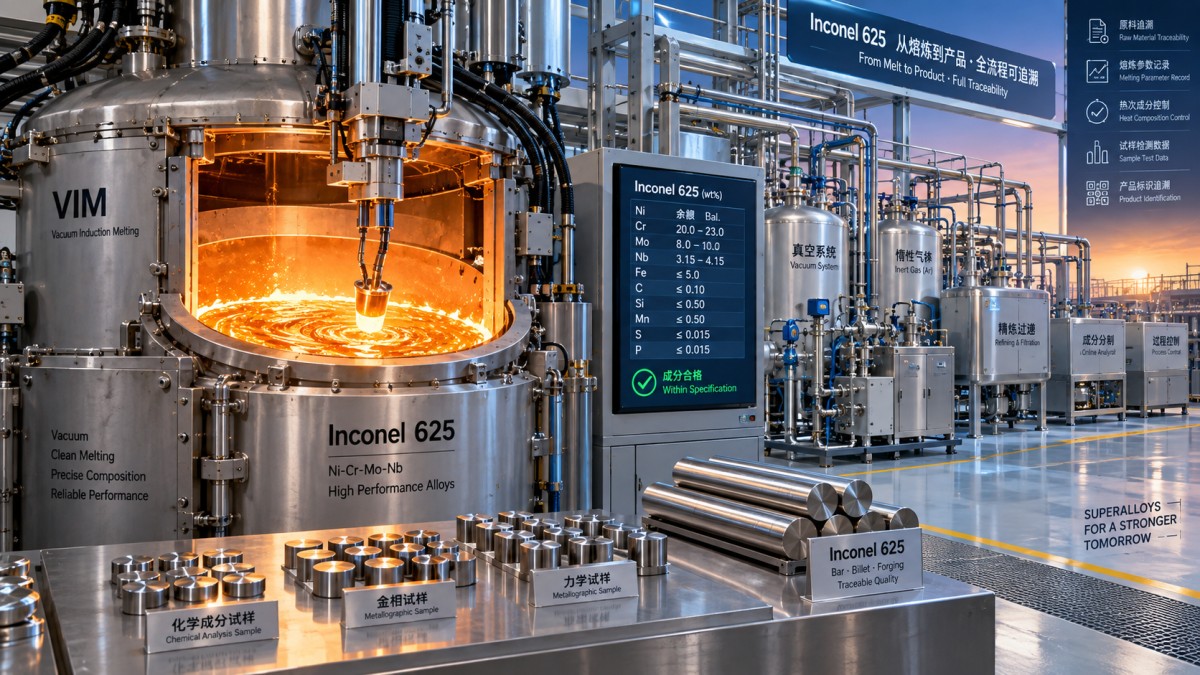
Real-time chemical analysis turns melting from an estimate into a controlled adjustment process. Samples are taken at defined stages, prepared to avoid surface contamination, and analyzed with methods appropriate to the element and required accuracy. Optical emission techniques are widely used for rapid melt control, while other analytical methods may be needed for elements that require lower detection limits or independent confirmation.
A sound control plan distinguishes between a process sample and a release sample. The process sample supports trimming decisions. The release sample documents the chemistry of the heat after final adjustment and adequate homogenization. Treating these as interchangeable creates a common source of confusion, particularly when a late addition has not fully mixed or when sample preparation differs between stages.
Trend review is as useful as the individual result. If multiple heats repeatedly require the same correction, the issue may lie in charge assumptions, actual recovery, calibration, furnace practice, or the stated chemistry of an addition material. Repeatedly trimming the same element without investigating the pattern can conceal a weakening process rather than demonstrate effective control.
Element relationships that require context
Chromium and molybdenum are often viewed primarily through corrosion resistance, but their values must be interpreted with the complete composition. Niobium contributes to strengthening and microstructural behavior, while iron, carbon, silicon, manganese, phosphorus, sulfur, and residual elements can influence processing and service performance even when they are secondary targets. Meeting a minimum molybdenum value does not offset a chemistry balance that has shifted elsewhere.
For welded equipment, chemistry control must be connected to the actual joining route. Base-metal analysis alone does not describe the composition of weld metal, dilution zones, or repair areas. A component may contain compliant parent material and still need separate verification of filler-metal identity and weld procedure controls. This distinction is particularly important where corrosion performance depends on a continuous, homogeneous alloy surface.
Heat-to-heat repeatability is different from specification compliance
Two heats can both comply with the same stated limits yet behave differently during forming, welding, machining, or corrosion exposure because they occupy different positions inside the allowed range. That does not automatically indicate nonconformance. It does mean that internal aim ranges are valuable when a product has a demanding downstream route.
For example, a fabrication involving extensive welding and severe chloride exposure benefits from a stable approach to the key corrosion-related elements and low impurity control. A heat intended for atomization into powder requires additional attention to cleanliness, particle production conditions, and lot segregation after melting. The chemistry certificate remains necessary, but it is not a substitute for controls specific to the conversion process.
In powder applications, the starting melt chemistry must remain linked to the powder lot, because particle-size distribution and flow behavior do not prove alloy identity. For applications such as additive manufacturing, corrosion-resistant cladding, or repairs of high-temperature components, Nickel-Based Superalloy Powders should be evaluated with the powder certificate, lot traceability, and the qualified processing parameters rather than by grade name alone.
Records should reconstruct the heat without assumptions
A useful heat record connects raw-material lots, charge weights, furnace or vessel identification, melt and refining stages, sample identifiers, analysis results, additions, retest results, and final disposition. The record should show whether the reported chemistry came from a final representative sample and whether any correction was made after the first analysis.
Traceability needs to continue through remelting, casting, forging, rolling, annealing, cutting, and shipment. When heats are split into multiple product lots, each lot must retain the heat reference. When different heats are combined in a finished assembly, material identification should remain visible or documented at the joint level. A certificate that states a heat number is of limited value if the physical material cannot be tied back to that number after processing.
Where composition reviews are commonly misread
A single certificate value should not be read as proof that all material in an assembly is equivalent. Product form matters. Plate, bar, strip, weld overlay, powder, and finished machined parts have different conversion histories and possible sources of variation. The analysis also needs to match the applicable material specification and condition; comparing results against an unrelated product-form requirement can create a false rejection or a false acceptance.
Another weak practice is to focus only on major alloying elements while ignoring residuals and interstitials. A heat can look favorable in nickel, chromium, molybdenum, and niobium yet warrant investigation when low-level contaminants are inconsistent with the intended service or processing route. Conversely, a value near an internal target is not automatically a problem when it remains within the approved range and the rest of the heat history is stable.
Composition control between heats is therefore a disciplined chain: known inputs, repeatable melting practice, representative analysis, justified corrections, and records that preserve the link from charge to delivered material. When that chain is intact, chemical consistency becomes a verifiable property of the production system rather than an assumption based on a final certificate.
