

News
- ▶ How to Verify C276 Material Traceability from a Supplier
- ▶ Questions to Ask Before Ordering Hastelloy C276 Plate or Pipe
- ▶ Alloy Sheet Inspection: Thickness, Surface Finish and Traceability
- ▶ Preventing Surface Contamination When Cutting Alloy Sheet
- ▶ Alloy Sheet for Chemical Tanks: Matching Grades to Process Media
Message
Alloy Sheet Inspection: Thickness, Surface Finish and Traceability
An alloy sheet is ready for acceptance only when its measured dimensions, surface condition and material records meet the requirements specified for the order and intended fabrication. A sheet can look clean but be too thin, carry the wrong heat identification, or have a surface defect that becomes a crack during forming. Inspection should bring those checks together before the material is released for use.
Start with the purchase order, drawing and applicable material specification. These documents establish the alloy grade, product form, thickness, finish, testing requirements and any additional customer conditions. Nominal thickness alone is not an acceptance limit: the permitted variation depends on the applicable requirements and, in some cases, the sheet dimensions and manufacturing condition.
Set the acceptance criteria before measuring
A material specification and a dimensional tolerance standard may serve different purposes. One may define chemical composition, mechanical properties and delivery condition; another may establish permissible dimensional variations. The purchase order or drawing can also impose additional requirements. Identify which documents apply to the exact sheet grade, product form and condition, then use the specified editions and any agreed supplementary requirements.
Record the inspection plan before opening the bundle. It should state how sheets are selected, where measurements are taken, which instruments are used, and how results will be recorded. Where the order does not define sampling, agree on an approach appropriate to the application and risk. Sampling can support a receiving decision, but it does not establish that every unmeasured location or sheet conforms.
Pay particular attention to minimum thickness requirements for components that will be formed, machined or exposed to corrosion. A sheet that meets its purchase tolerance may still be unsuitable if the fabrication allowance or design minimum was not included when the material was ordered.
Measure thickness where variation matters
Use a calibrated instrument with a suitable measuring range and resolution. A micrometer is commonly used for accessible sheet edges and surfaces; other methods may be appropriate where access, size or the inspection plan requires them. Check the instrument before use, keep the measuring faces clean, and avoid excessive force that could distort thin material or affect the reading.
Take readings at locations defined by the applicable tolerance rules and inspection plan, including positions across the width and along the length where accessible. Edge readings are useful, but they may not represent the center of a wide sheet. Do not move measurement points inward or outward simply to obtain a passing result: some dimensional requirements specify where measurements count.
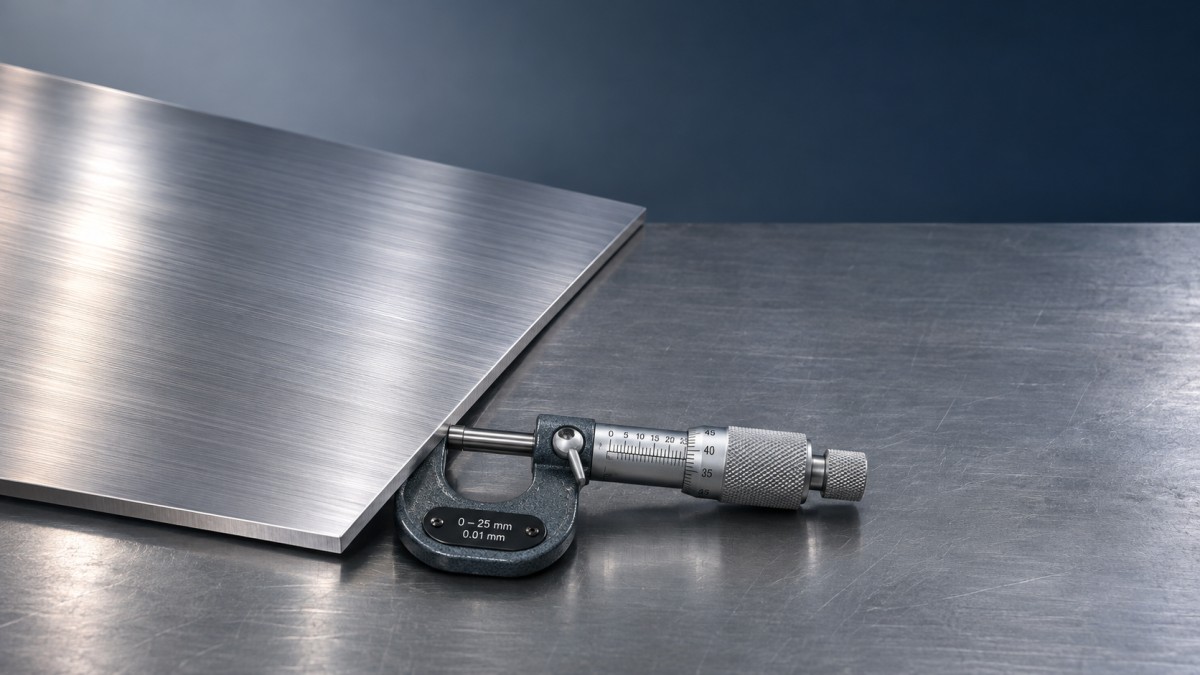
Record individual readings and their locations, not just an average. An average within tolerance can conceal a local low reading. Compare each applicable reading with the permitted limits, and distinguish a reading outside tolerance from one that is close to a limit but still conforming. Measurement uncertainty and instrument condition matter when a result is near the boundary; follow the agreed decision rule rather than rounding a borderline value into acceptance.
If a low spot is found, mark its location and hold the affected material. Check for burrs, debris or an instrument issue, then remeasure using the approved method. Do not grind the area to make it look uniform: removing material can make a thickness problem worse and may erase evidence needed for disposition.
Judge surface finish against the intended use
Inspect both faces under lighting that makes changes in texture and reflected light visible. Depending on the specified finish and service, relevant conditions can include scratches, dents, pits, seams, laminations, scale, discoloration and embedded contamination. Note the location, extent and appearance of each suspect area so it can be evaluated against the applicable acceptance criteria.
Not every visible mark is a rejectable defect. A superficial handling mark on a noncritical face may be acceptable under the order, while a similar-looking indication on a sealing surface or a sheet destined for severe forming may require closer review. Conversely, a bright, uniform appearance is not proof that the surface is free of harmful discontinuities.
Where surface roughness is specified, measure it using the required parameter and method. A visual comparison alone cannot demonstrate compliance with a numerical roughness limit. Direction also matters: rolled texture and scratches can affect both the measurement and the finished component, so follow the specified measurement orientation and reporting requirements.
Protective film, oil and packaging can hide damage. Remove or lift protection as needed for inspection without introducing new scratches or contamination, then restore suitable protection for storage. Suspect cracks, deep pits or lamination-like indications may require additional examination under an agreed procedure. Any repair or blending should be authorized, controlled and followed by a thickness check where material was removed.
Traceability must follow the physical sheet
Traceability connects a piece of material to its identity and supporting records. At receipt, compare the sheet or bundle markings with the purchase order, packing documents and material test certificate. Review the grade or UNS designation, heat number, product form, dimensions, delivery condition and specified test results. A certificate should be assessed against the actual order requirements; its presence alone does not establish compliance.
Check that the reported chemical and mechanical results correspond to the specified requirements and that any required testing or inspection is documented. Certificate type, inspection authority and supporting records should be those called for in the contract. Do not assume that an ISO certificate for a management system, for example, replaces product-specific test evidence.
Traceability is most vulnerable after bundles are opened and sheets are cut. Transfer identification to individual sheets and remnants before the original marking is removed, using a method permitted for the material and application. Maintain a record linking each new identifier to the original heat and relevant inspection documents. Keep unidentified pieces segregated until their status is resolved through the applicable procedure.
Positive material identification can help detect a grade mix-up, but its scope matters. An instrument may identify selected alloying elements without verifying every composition limit, heat treatment condition or mechanical property. A matching reading therefore supports identification; it does not replace the required certificate or prove that the sheet belongs to a particular heat.
Keep sheet and tube requirements separate
Related alloy products may share a grade name while being governed by different product-form requirements. For example, Monel Alloy Tubes are available in Monel 400 and Monel K-500 for applications that include marine and chemical equipment. Tube dimensions and inspection requirements should not be substituted for those specified for sheet, and the two grades should not be treated as interchangeable merely because both carry the Monel name.
Release, hold or reject
Release material only after the required dimensional, surface and documentation checks are complete and any discrepancies have been resolved. Record the inspected material identifiers, results, applicable acceptance criteria and disposition so the decision remains understandable after the sheet enters production.
When a requirement is not met or identity is uncertain, segregate and label the affected material to prevent unintended use. A disposition may involve additional inspection, supplier correction, an authorized concession or rejection, depending on the issue and the contract. A concession should identify the affected material and the specific deviation; it should not silently change the acceptance criteria for the rest of the order.
